7 Communication Mistakes U.S. Buyers Make When Sourcing from Asia
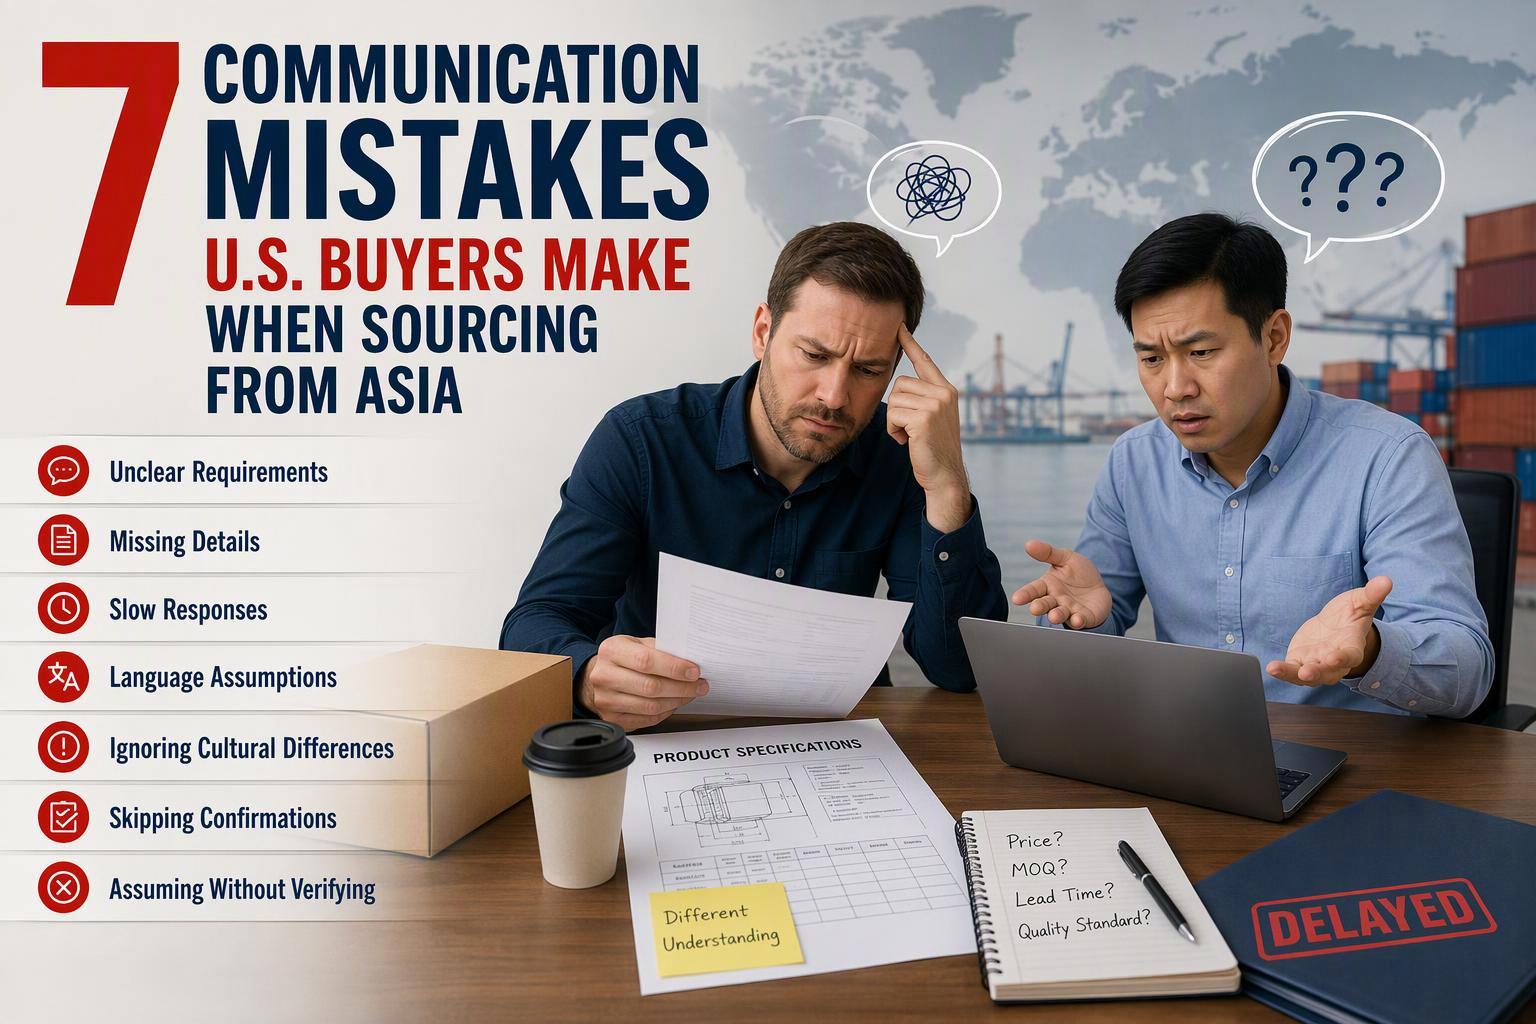
Most sourcing problems that reach the buyer's desk as a defect, a late container, or a surprise invoice started as a sentence someone wrote too quickly. This guide walks through seven communication mistakes U.S. buyers make with Asian suppliers, what each one costs in practice, and the specific fix that keeps it from repeating.
1.Why Communication Matters in Overseas Sourcing
A U.S. buyer sends a product photo and a few basic specifications to an overseas supplier. The supplier confirms the order, and everyone feels aligned. Then the shipment arrives and the material, dimensions, or finish don't match what the buyer pictured.
The gap rarely comes from bad faith on either side. It comes from a message that left room for interpretation, and a factory that filled that room with its own defaults. A photo shows shape, not alloy. "100 mm" names a target, not an acceptable range. "Corrosion resistant" describes an outcome, not a test.
Each of the seven mistakes below follows the same pattern: an unanswered question in the buyer's message becomes an assumption in the factory's process, and that assumption hardens into steel, coating, and packaging before anyone notices. The cost shows up later as rework, air freight, missed retail windows, or a customer relationship that takes years to rebuild. The fix in every case is cheap at the start and expensive at the end, which is why the sections below pair each example with the specific document, question, or cadence that closes the gap.
2.Sending Vague Product Specifications
The mistake: A buyer sourcing a custom metal bracket specifies a dimension of 100 mm and nothing else. The factory produces to its own shop default, the bracket arrives, and it won't seat in the assembly.
The buyer believed they had communicated a size. What they actually communicated was a nominal target with no boundary. Every manufacturing process carries variation, and tolerance defines how much deviation a part can have before it stops working. A nominal 100 mm with a tolerance of ±0.5 mm, for example, accepts anything from 99.5 mm to 100.5 mm. That half-millimeter is the difference between a bracket that drops into place and one that needs a file, a hammer, or a scrap bin.
Factories do not guess at tolerance out of laziness. They apply the general tolerance block on their own drawings or their customary process capability, because a tighter range usually means more precise machining, slower cycle times, and additional inspection. Tolerance costs money, so a factory that receives no instruction will default to the loosest range that still lets it ship. If the mating hole on your assembly needs an interference fit or a clearance fit, only you know that, and only if you say so.
The fix: Send a package, not a message. For a custom bracket, that means:
- A dimensioned 2D drawing with a title block showing part number, revision, material grade, and finish
- Material called out by industry designation (6061-T6 aluminum, 304 stainless) rather than a generic word like "aluminum"
- Tolerances on every critical feature, with a general tolerance block for everything else
- The application: what the part mounts to, what load it carries, whether it sits outdoors
- Acceptance criteria, including which dimensions get inspected and how
Then ask for written confirmation of the critical parameters before the factory cuts material. A short reply that restates your tolerance, material, and finish in the supplier's own words catches misreadings while they are still free to fix. If the supplier proposes a looser tolerance or a substitute grade, that is useful information, not an insult. Evaluate it against the function of the part and answer in writing.
3.Assuming Suppliers Understand Your Requirements
The mistake: A U.S. building materials buyer specifies that hardware must have a particular level of corrosion resistance. The factory reads "corrosion resistant" and applies its standard plating. The finished hardware passes the factory's own idea of acceptable and fails the project's environmental requirements.
This mistake differs from vague specifications in an important way. The buyer here may have written a great deal, but the requirement lived in the buyer's head as a performance outcome rather than in the document as a testable condition. "Corrosion resistant" means different things on a bathroom fixture, a coastal installation, and an industrial wash-down environment. The factory cannot see your installation site, so it applies the coating it applies every day.
Corrosion performance is also a specification with real technical structure. Salt spray testing under ASTM B117 creates a controlled corrosive environment, but the standard itself does not prescribe exposure periods for a specific product or how to interpret results, and the standard notes that predicting natural-environment performance from salt spray alone has seldom been correlated. In practice, buyers and suppliers agree on a coating class and a test duration, then treat the result as an auditable check rather than a guarantee. A plating specification that names the coating type, thickness range, and the hours it must survive turns a vague wish into something a factory can quote and an inspector can verify.
The fix: Ask the supplier to confirm your requirements item by item, in writing, and to flag anything it cannot meet. A useful confirmation covers:
- Each specification, restated in the supplier's words
- The test method and standard that will verify each one
- Any requirement the factory cannot satisfy, stated plainly before the order
- The documents that will accompany shipment (material certificates, inspection reports, coating thickness records)
Record the agreed items in a drawing, a specification table, or a signed specification sheet. A signed document gives both sides the same reference point when a question arises months later, and it removes the ambiguity that lets a factory substitute a standard finish for a project-specific one.
4.Misunderstanding Lead Time and Delivery Dates
The mistake: A factory says "30 days delivery." The buyer hears a date the goods will arrive. The factory means something narrower, and the difference surfaces only when the container is still on the water in week seven.
Lead time is not one number. It is a chain of stages, and the phrase "30 days" can refer to any of them. A U.S. distributor who needs product in June receives a 30-day quote that actually means 30 days to complete production after the deposit clears and the drawings are approved. Shipping and customs sit outside that window entirely.
The stages that commonly hide inside a single quoted figure include:
- Order trigger: what starts the clock. It might be order confirmation, a cleared deposit, sample approval, or confirmed raw materials. Naming the trigger in writing often explains the first week or two of any gap.
- Queue time: the wait before your job reaches a production line. A plant quoting 25 production days may not begin those days for three weeks if its schedule is full.
- Production time: the actual run.
- Ship-ready date: when goods leave the factory, which is not the same as the sailing date.
- Transit and clearance: ocean freight from China to the U.S. West Coast runs roughly 14 to 18 days port to port, and 25 to 35 days to the East Coast. Customs release typically takes 24 to 48 hours when an entry clears without examination, and longer if CBP selects it for inspection. Add inland transport and warehouse receiving on top.
Stack those stages and a first order can easily run 35 to 75 days from production start to a West Coast warehouse, or 50 to 90 days to the East Coast. None of that is unusual; it is simply invisible when the quote says "30 days."
The fix: Break the single number into four confirmed dates, and put them in the purchase order rather than in an email thread:
- Production start date, with the trigger condition named
- Production completion date
- Ship-ready date
- Estimated arrival at your U.S. destination, with the shipping terms stated
Separate the dates that bind the supplier from the dates that are estimates. A production completion date is something a factory can commit to. An arrival date depends on carriers, ports, and customs, so treat it as a planning figure with a buffer. Also confirm which Incoterms rule governs the shipment, because the delivery point and the point where risk transfers change the meaning of every date on the page. For a June shelf date, work backward from arrival, not forward from the quote.
5.Discussing Important Changes Without Written Confirmation
The mistake: A buyer calls the supplier to change the color of a hardware accessory. The sales contact says yes. The production department keeps running the original purchase order, and the shipment arrives in the old color.
Verbal changes fail for a structural reason: the person who takes your call is rarely the person who sets up the machine. In most factories, sales or merchandising owns the customer relationship while a production manager owns the schedule and the work instructions. A phone call updates the relationship. It does not update the paperwork the line actually follows.
Changes also carry consequences that a quick yes ignores. A color change may require a new powder coat batch, a minimum order quantity, a masking change, or a longer cure. A material substitution may affect lead time and cost. When none of that gets discussed, the factory either absorbs a cost it did not quote or quietly reverts to the original spec.
The fix: Treat every change as a document, even a small one. A workable change record includes:
- A version number for the order or specification
- Exactly what changed, with the old and new values side by side
- The cost impact, if any
- The schedule impact, if any
- Who requested it, when, and why
- Approval status from both sides, with names and dates
The record should identify which parts, assemblies, or purchase order lines the change affects, so the factory knows the scope. Once both sides approve, the new version replaces the old one as the controlling document, and the factory confirms that production has switched to it. A one-page form sent by email and acknowledged in writing is enough. The point is not bureaucracy; it is that the production floor needs a piece of paper it can hold next to the work order.
6.Failing to Request Regular Production Updates
The mistake: A custom industrial parts order slips because raw material arrives late. The supplier knows about the delay but does not mention it. The buyer finds out when the ship date passes, by which point the U.S. customer's delivery schedule has already been promised and broken.
Factories tend to report good news early and bad news late. A supplier that is on schedule says so; a supplier that is behind often stays quiet until the gap becomes impossible to hide. Buyers who wait for updates therefore usually receive the update from before the problem started.
The cost of late notice compounds. A delay discovered in week two of a six-week build leaves room to expedite material, resequence the line, split the shipment, or renegotiate with the end customer. The same delay discovered in week five leaves only air freight, penalty clauses, and an apology.
The fix: Agree on the reporting rhythm before the order starts, and write it into the purchase order. A practical structure covers:
- Named checkpoints: material arrival, production start, first-off sample, mid-run, pre-shipment inspection, ship-ready
- Update frequency: for example, a short written status every week, plus a photo or inspection record at each checkpoint
- Format: a simple table showing planned versus actual dates for each checkpoint, with a note on any variance
- Escalation rule: who the supplier contacts, and how quickly, when a checkpoint slips or a risk appears
Dated photographs at material arrival, production start, and mid-run give you evidence at the moments that matter, which is more useful than a weekly message saying everything is fine. For high-value or schedule-critical orders, ask for the key inspection records alongside the progress report. A missed milestone is far easier to spot than a reassuring sentence, and it reaches you while you still have decisions to make.
7.Ignoring Time Zones and Communication Responsibilities
The mistake: A U.S. company sources cabinets, hinges, pulls, and other hardware from several factories. Each factory has a different contact person, a different working schedule, and a different idea of when to reply. A change confirmed with one supplier never reaches the buyer's own order file, and a detail falls through.
The time zone gap is the visible part of this problem. A buyer in Chicago who sends a question at 4 p.m. local time sends it at 5 a.m. the next day in China, so a same-day answer is impossible unless someone is working unusual hours. Add multiple factories, each with its own sales contact, production manager, and quality lead, and the number of communication threads multiplies faster than any one person can track.
A single order can involve a sales contact who owns the relationship, a production manager who owns the schedule, and a QC lead who owns inspection. When the buyer talks only to sales, information about the line and the inspection never enters the conversation. When three factories each route updates through a different person, comparing status across the program becomes guesswork.
The fix: Assign ownership on your side and set expectations on theirs.
- Name one sourcing coordinator who owns all supplier communication for the program, so every factory knows who to contact and every message lands in one place.
- Keep a single log of key items: open questions, confirmed changes, promised dates, and outstanding documents, organized by factory and order.
- Agree on response windows that respect the time difference. A 24-hour reply standard on business days is realistic; a same-day standard usually is not. State which hours overlap and how urgent issues get flagged.
- Build a multi-supplier tracker showing each factory's current stage, next milestone, and any open issue, reviewed on a fixed weekly rhythm.
With one coordinator and one tracker, a missed reply becomes visible within a day instead of surfacing at the port.
How to Improve Communication with Asian Manufacturers
Use a standardized RFQ template. Build one package you send to every supplier: drawing with revision, material grade and standard, critical dimensions and tolerances, finish and coating specification, quantity and batch requirements, certificate and inspection needs, destination, and application context. A complete package produces faster, more comparable quotes and fewer clarifying rounds. An incomplete one forces engineers on both sides to guess, and guesses turn into budget risk and first-article surprises.
Confirm specifications in writing. Ask the supplier to restate your requirements in its own words and to flag anything it cannot meet. Keep the confirmed version as the controlling document for the order. When a factory proposes an alternative material or finish, evaluate it against the part's function and answer in writing rather than letting silence count as approval.
Establish a single point of contact. One coordinator on your side, one named contact per factory, and a clear escalation path for problems. This is the simplest way to stop a detail from disappearing between two people who each thought the other had handled it.
Set clear production milestones. Put the production start trigger, completion date, ship-ready date, and estimated arrival into the purchase order, along with the checkpoints where you expect an update. Distinguish binding commitments from estimates so both sides know which dates carry weight.
Keep records of all changes. Version every change, record cost and schedule impact, and obtain approval from both sides before production switches over. A change that lives only in a phone call is a change that may never happen, or may happen twice.
Simplify Your Sourcing Communication with COSTLOU
Managing overseas suppliers doesn't have to be complicated.
COSTLOU helps U.S. businesses communicate product requirements, coordinate manufacturers, and keep sourcing projects organized, from initial inquiries to delivery. That means one point of contact across factories, specifications confirmed in writing, milestones tracked against the purchase order, and changes recorded so nothing depends on a phone call someone half remembers.
If you are sourcing hardware, components, or custom parts from Asia and want the communication handled with the structure described above, visit COSTLOU to start the conversation.
One Point of Contact. Smarter Sourcing Across Asia.